 Nuclear fusion · Process plants and instrumentation
Cooling skids for the MAST-U tokamak
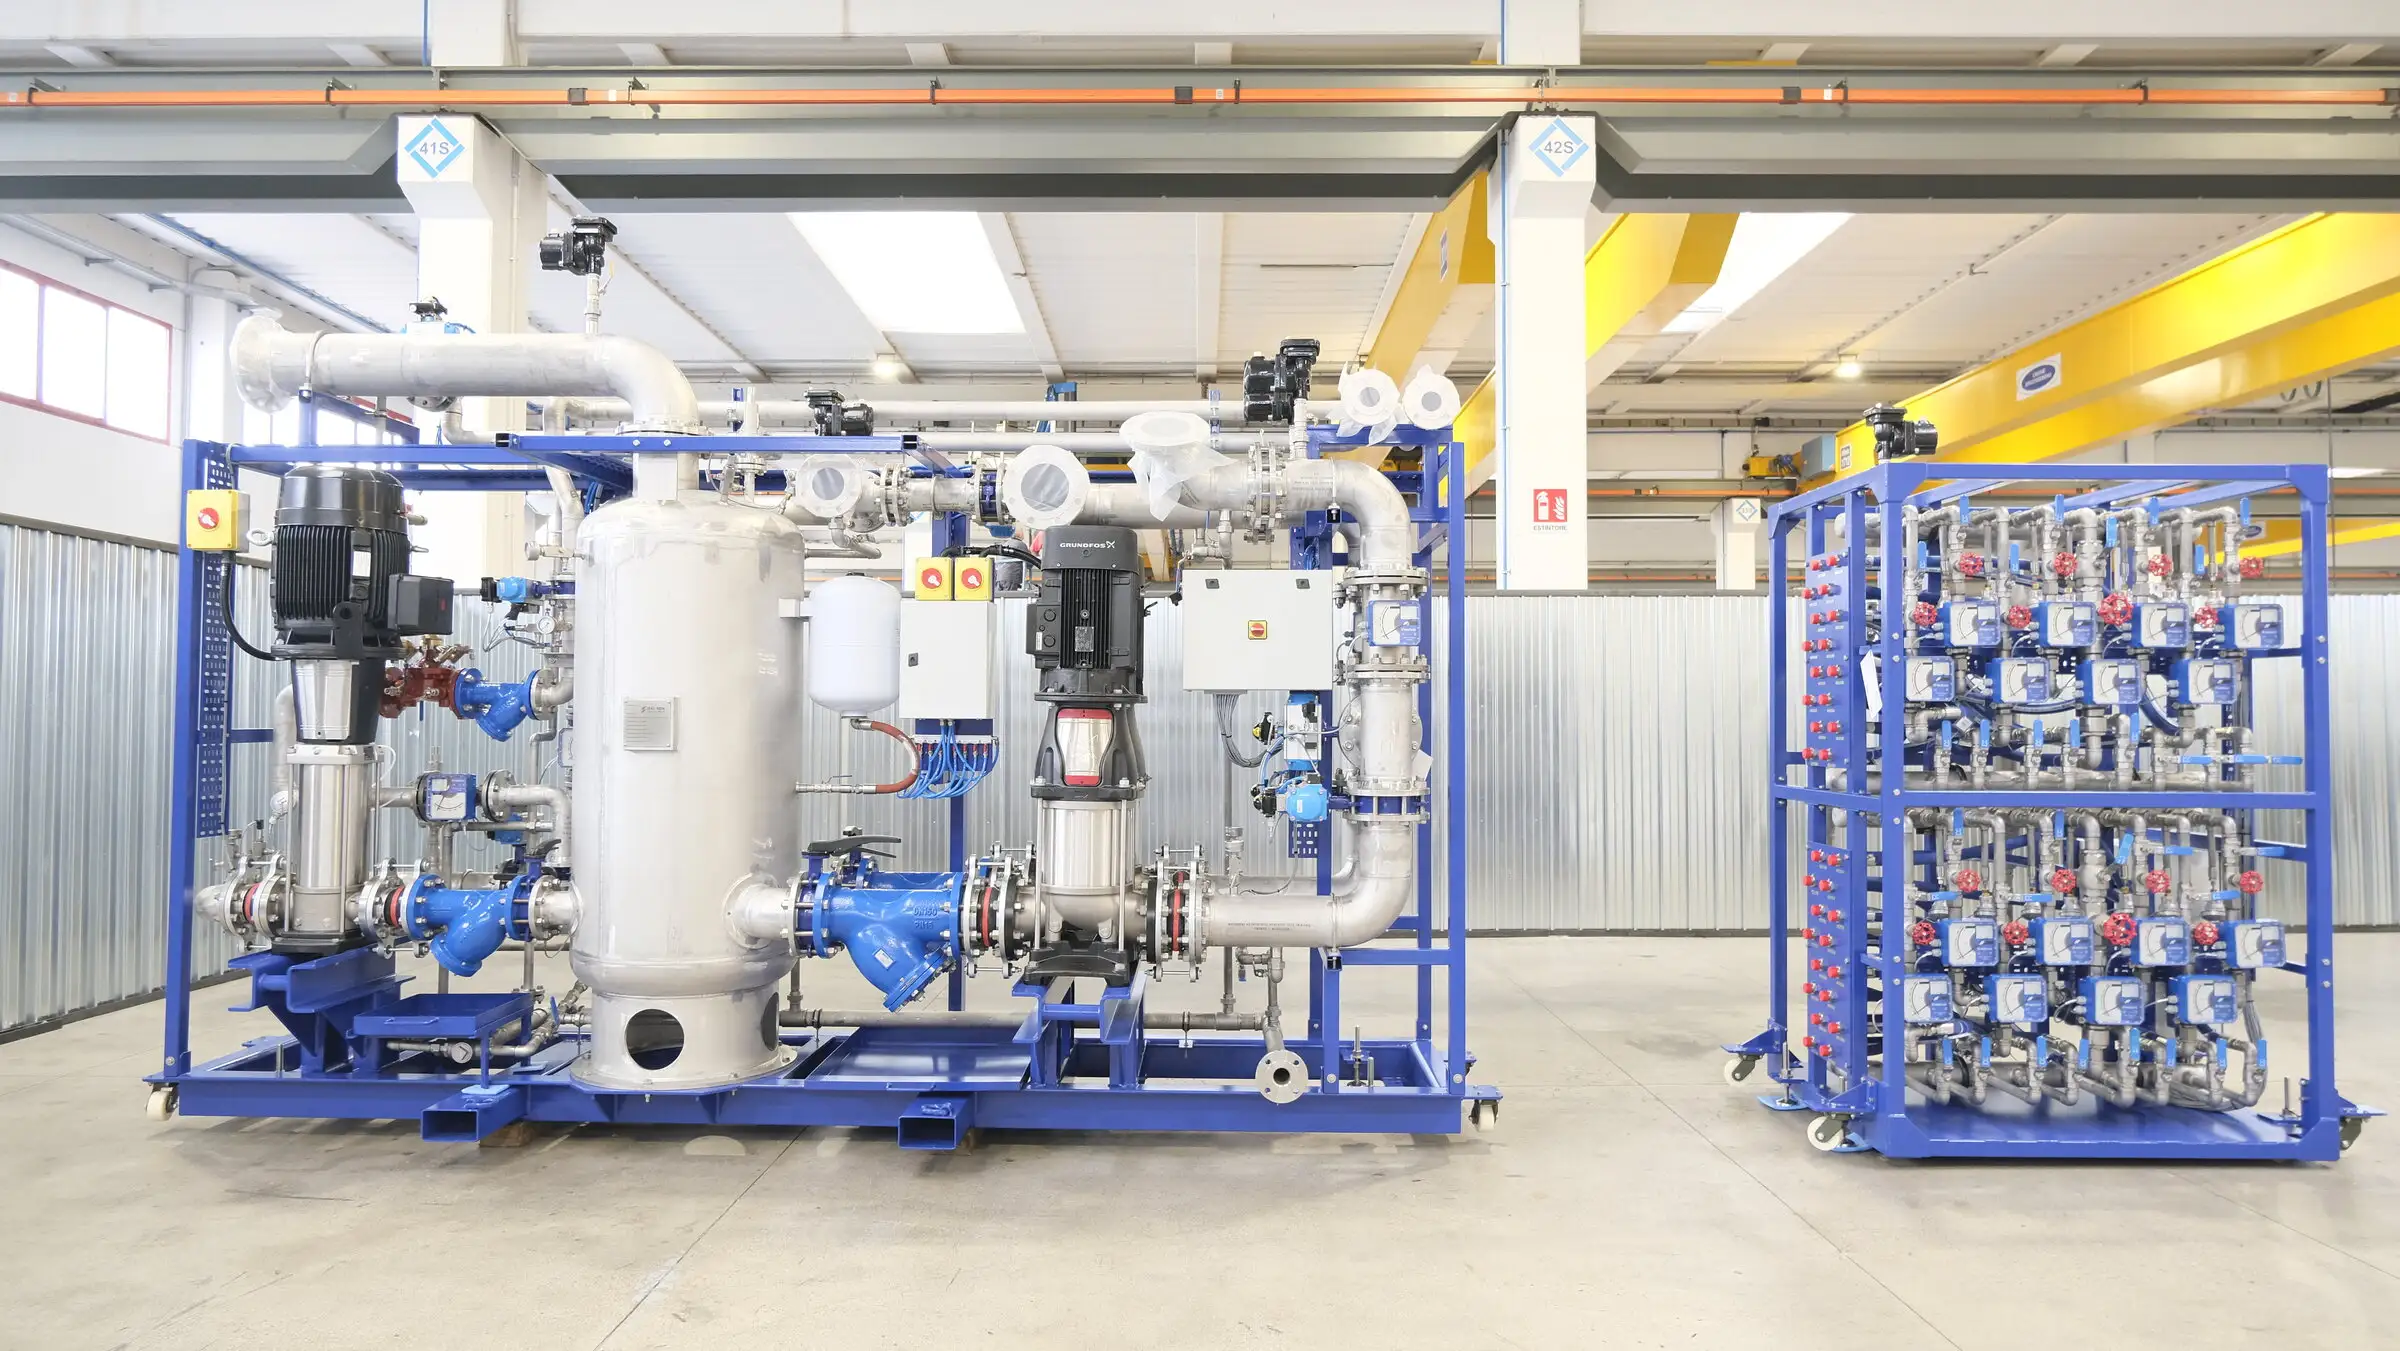
Three skids for the demineralised water circuit that cools a Neutral Beam Injector: pumping, filtration, regulation and flow measurement on sixteen independent lines.
- 3
- Skids delivered as complete packages
- 16
- Flow measurement and regulation lines
- 750 l
- Stainless steel tank
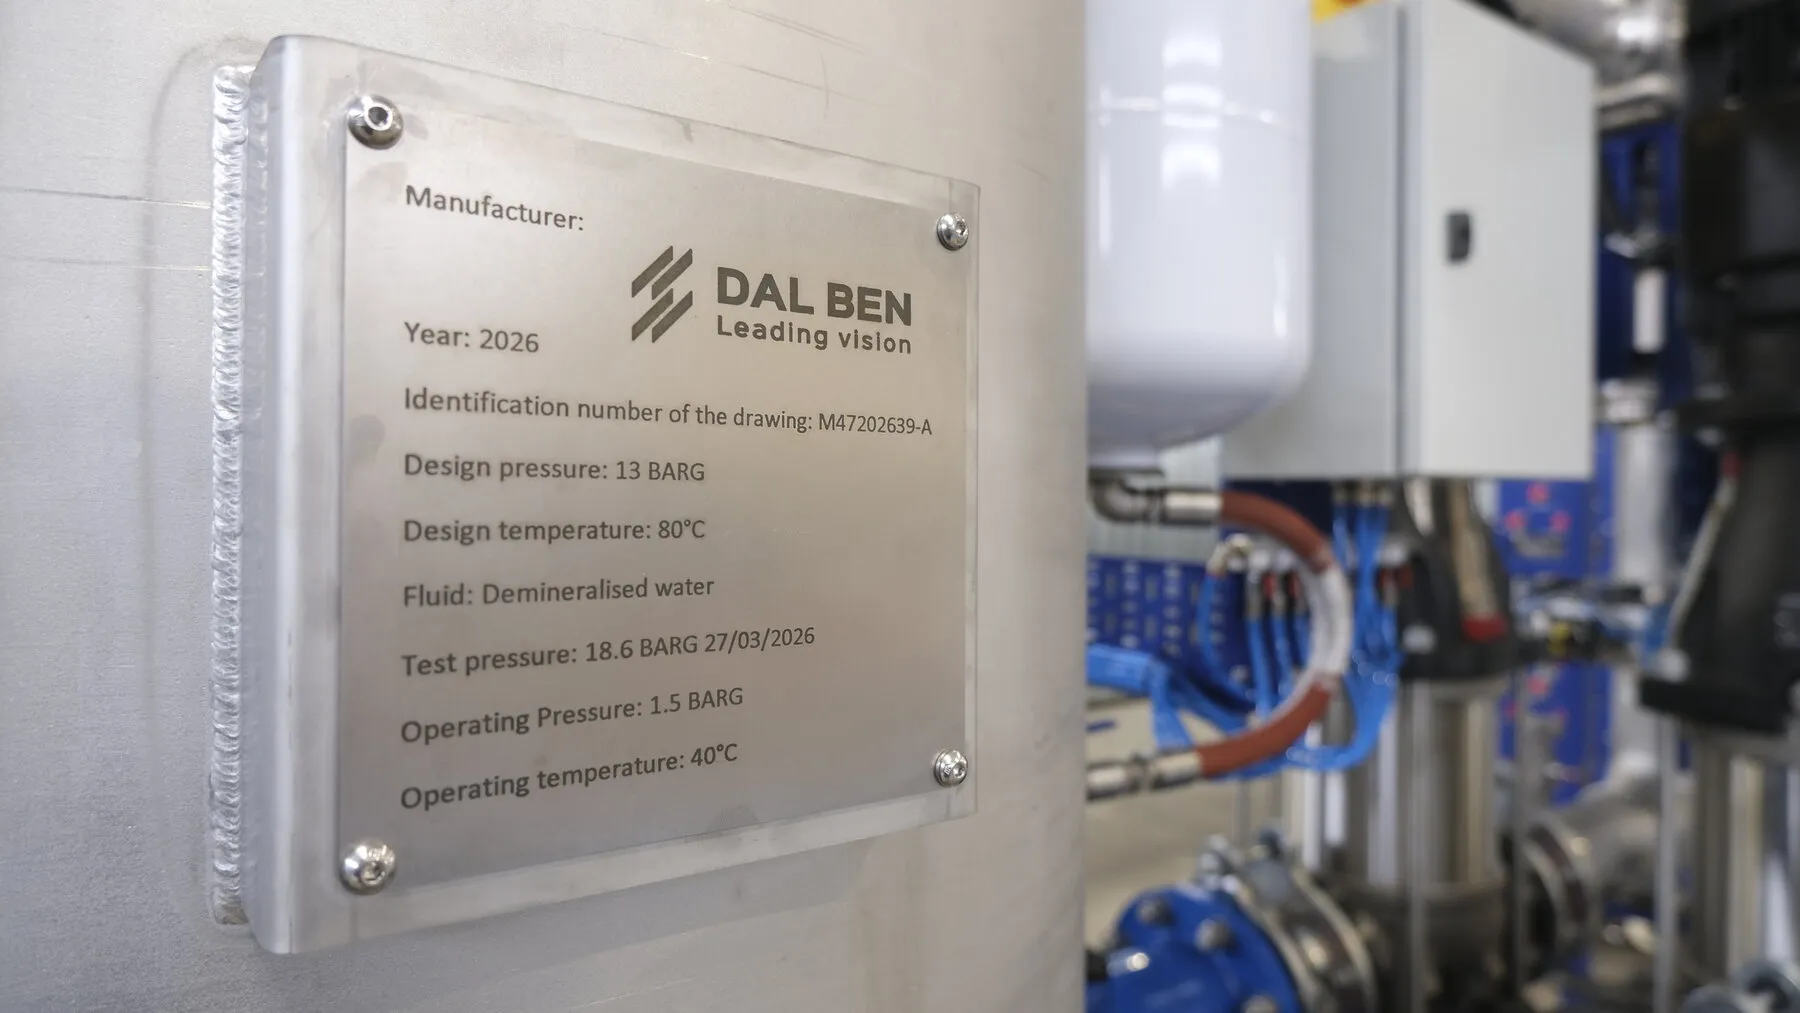
- 18.6 barg
- Hydrostatic test with no pressure drop
00
The circuit
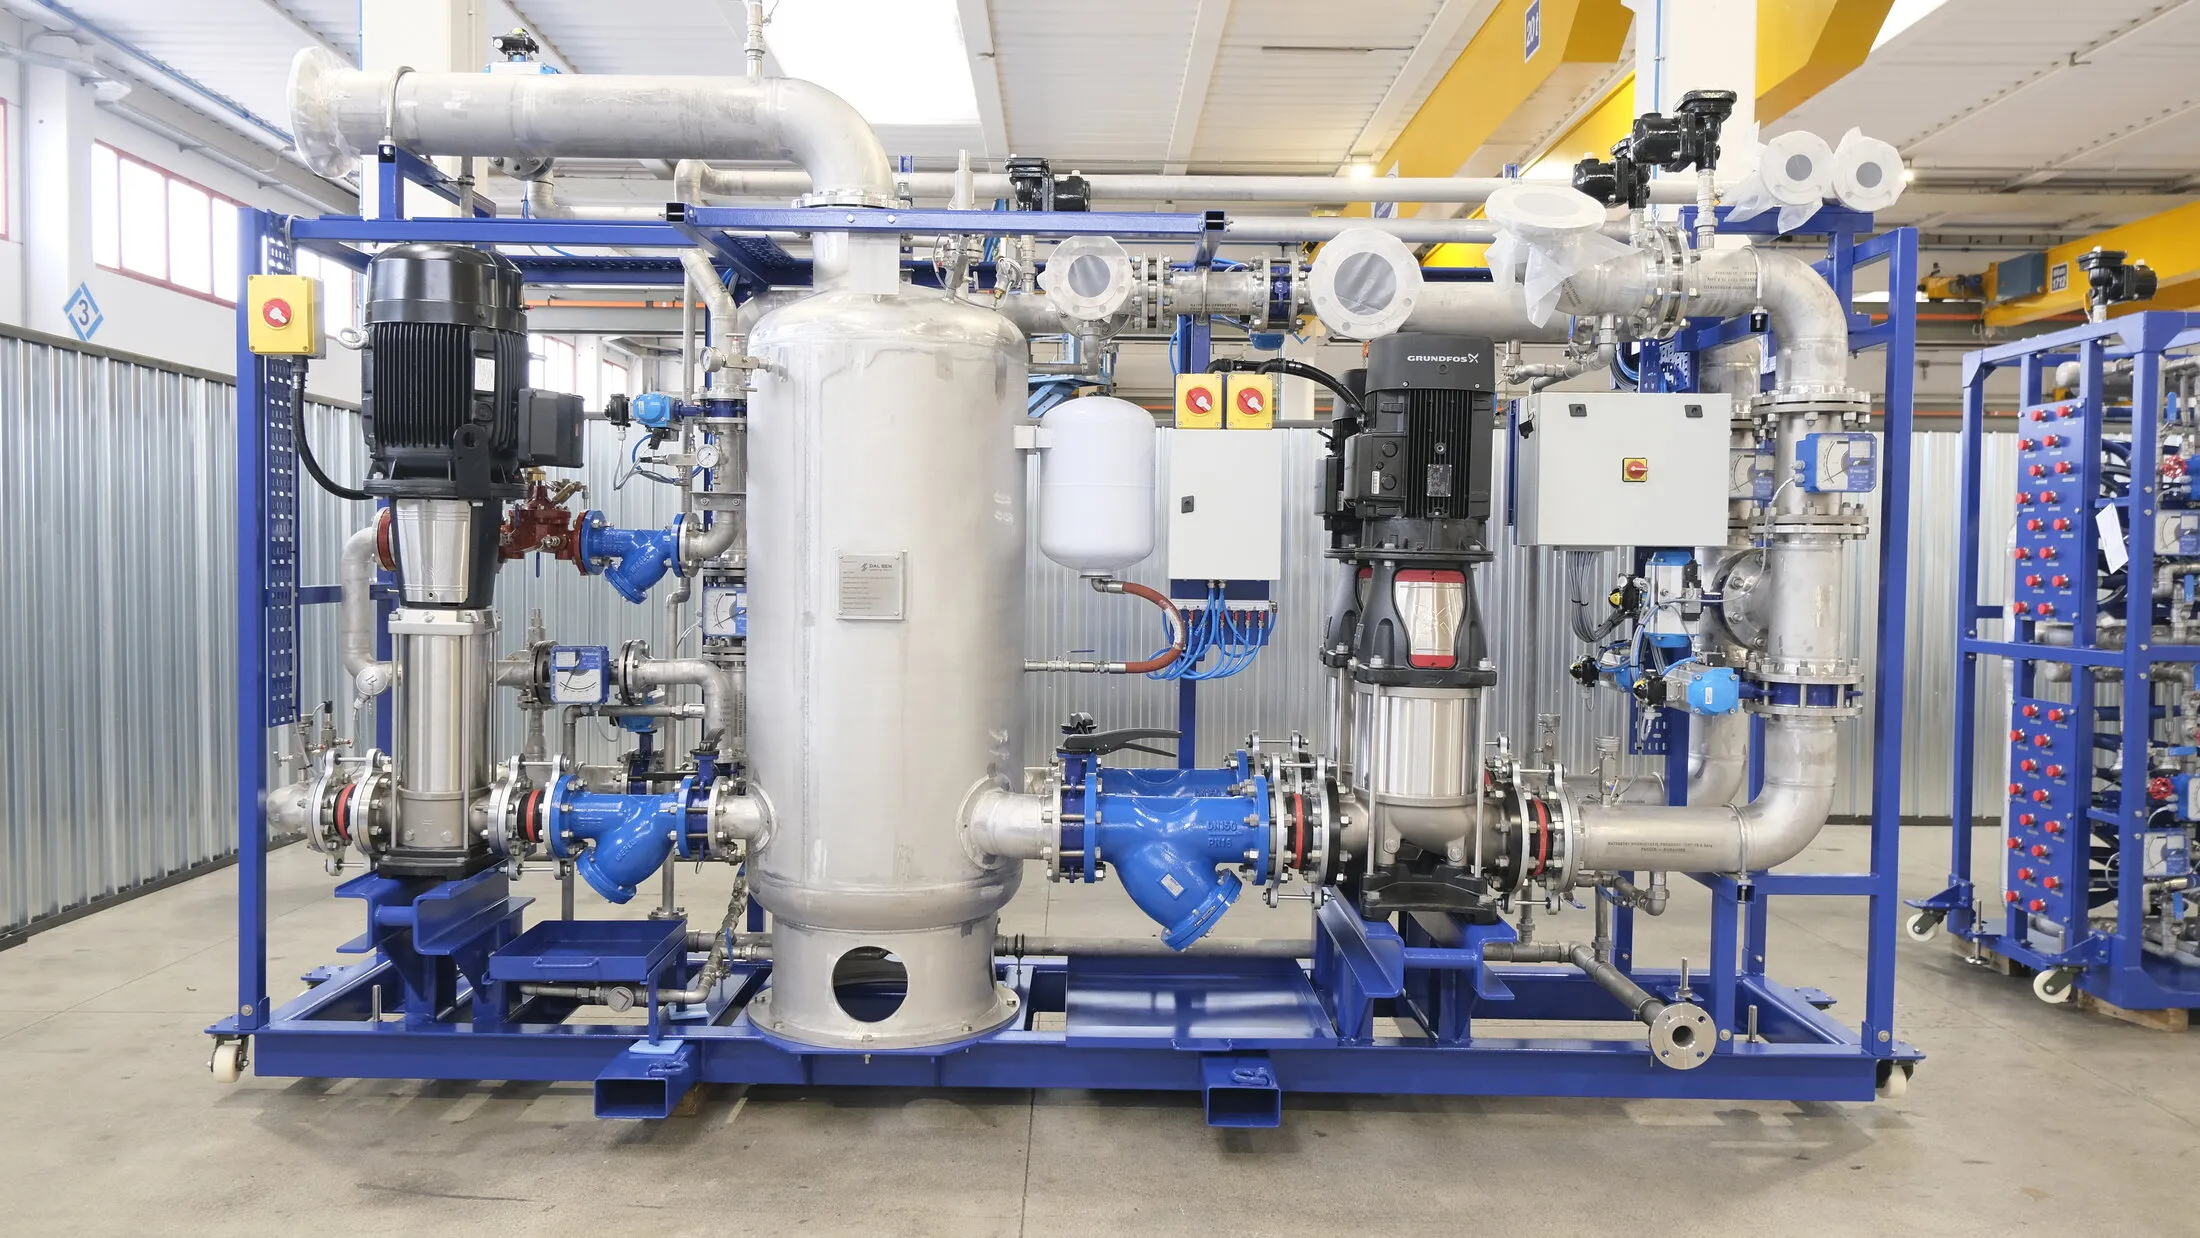
MAST Upgrade is a spherical tokamak for nuclear fusion research. Its Neutral Beam Injector uses a dedicated demineralised water circuit, split across three skids.
- Pumping skid: 750-litre stainless steel tank, three vertical multistage pumps with Y-strainers, expansion vessel, pneumatic control valves, safety valves, 4-20 mA flow meters and automatic flow control valve
- Supply and return manifold: a DN100 flange distributes the flow across sixteen lines; on the return each line has a flow meter, balancing valve, isolation valve and thermocouple
- A smaller measurement manifold
01
Control, instrumentation and wiring
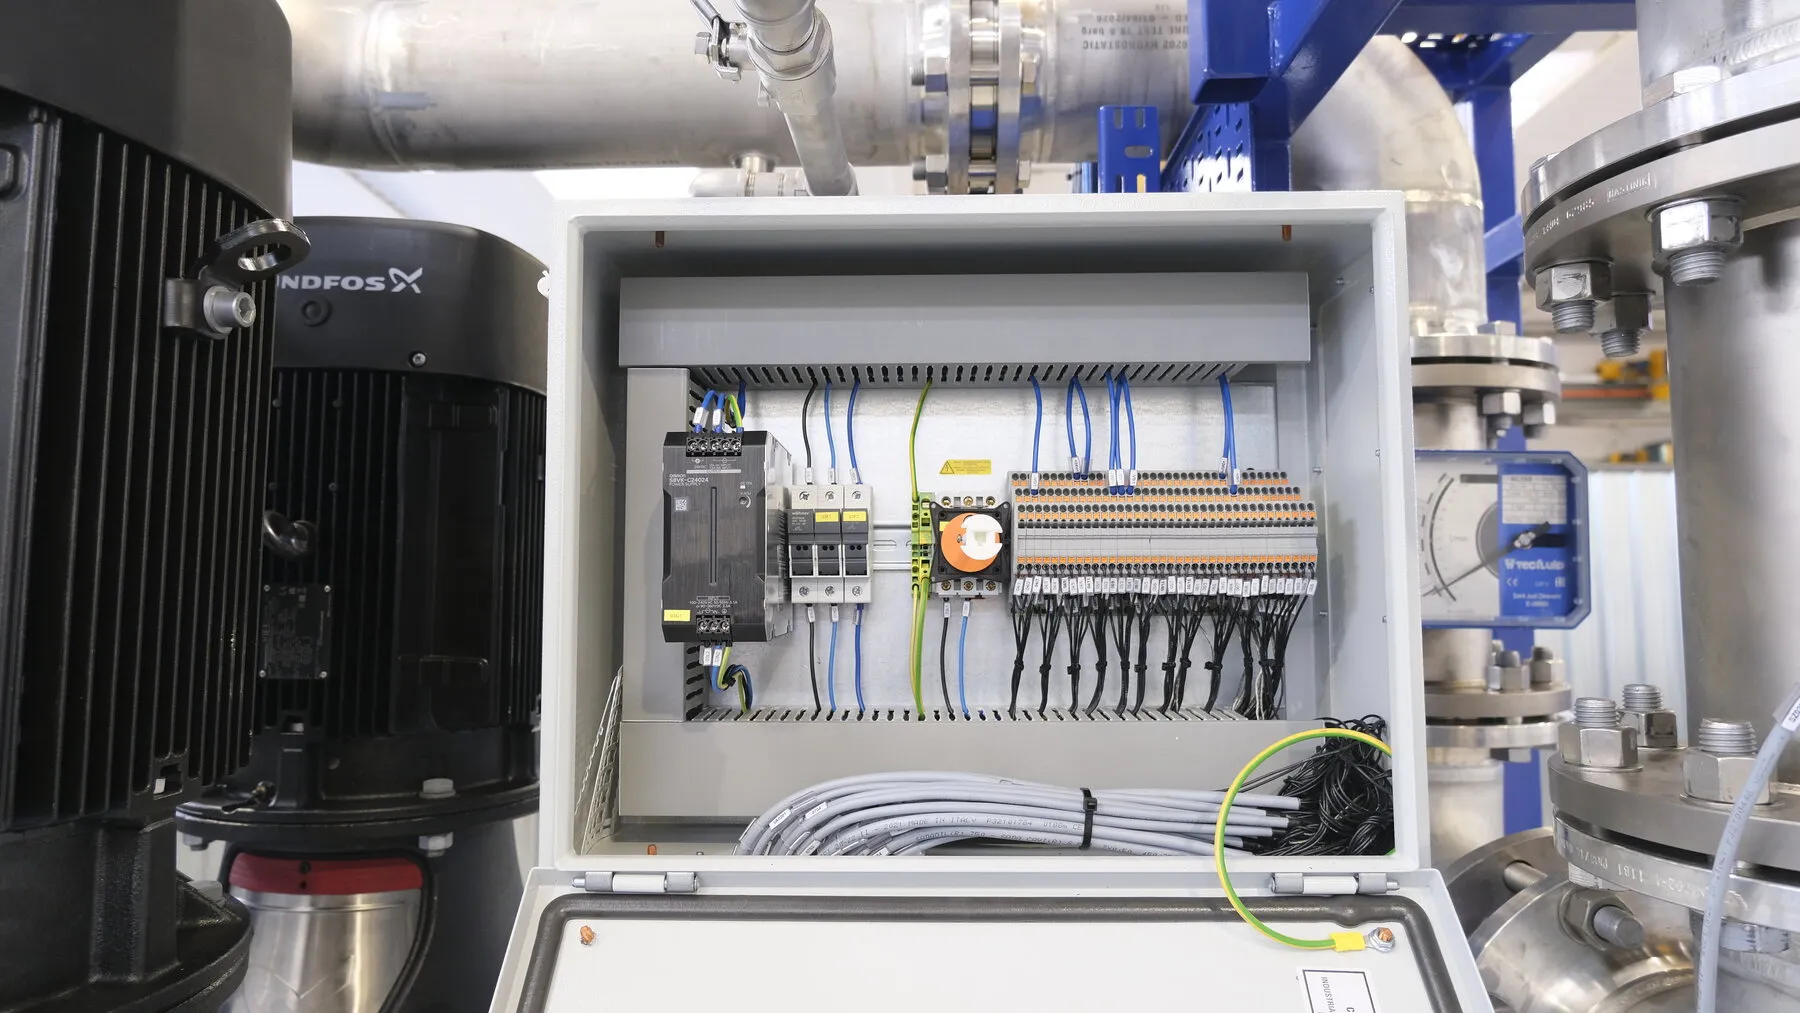
- Pressure or flow control and temperature control
- Flow, pressure and temperature instrumentation
- Pneumatic control valves
- Junction boxes with DIN-rail terminal blocks
- Cable routing and signal identification
Factory functional tests included a point-to-point check of the sensor signals, energising the pneumatic circuit and operating the valves.
02
Welding, inspection and testing
- Piping spools in 304L stainless steel, materials certified EN 10204 3.1
- Welding documentation approved by a third-party body
- 100% non-destructive testing on the welds: visual, dye penetrant and radiographic
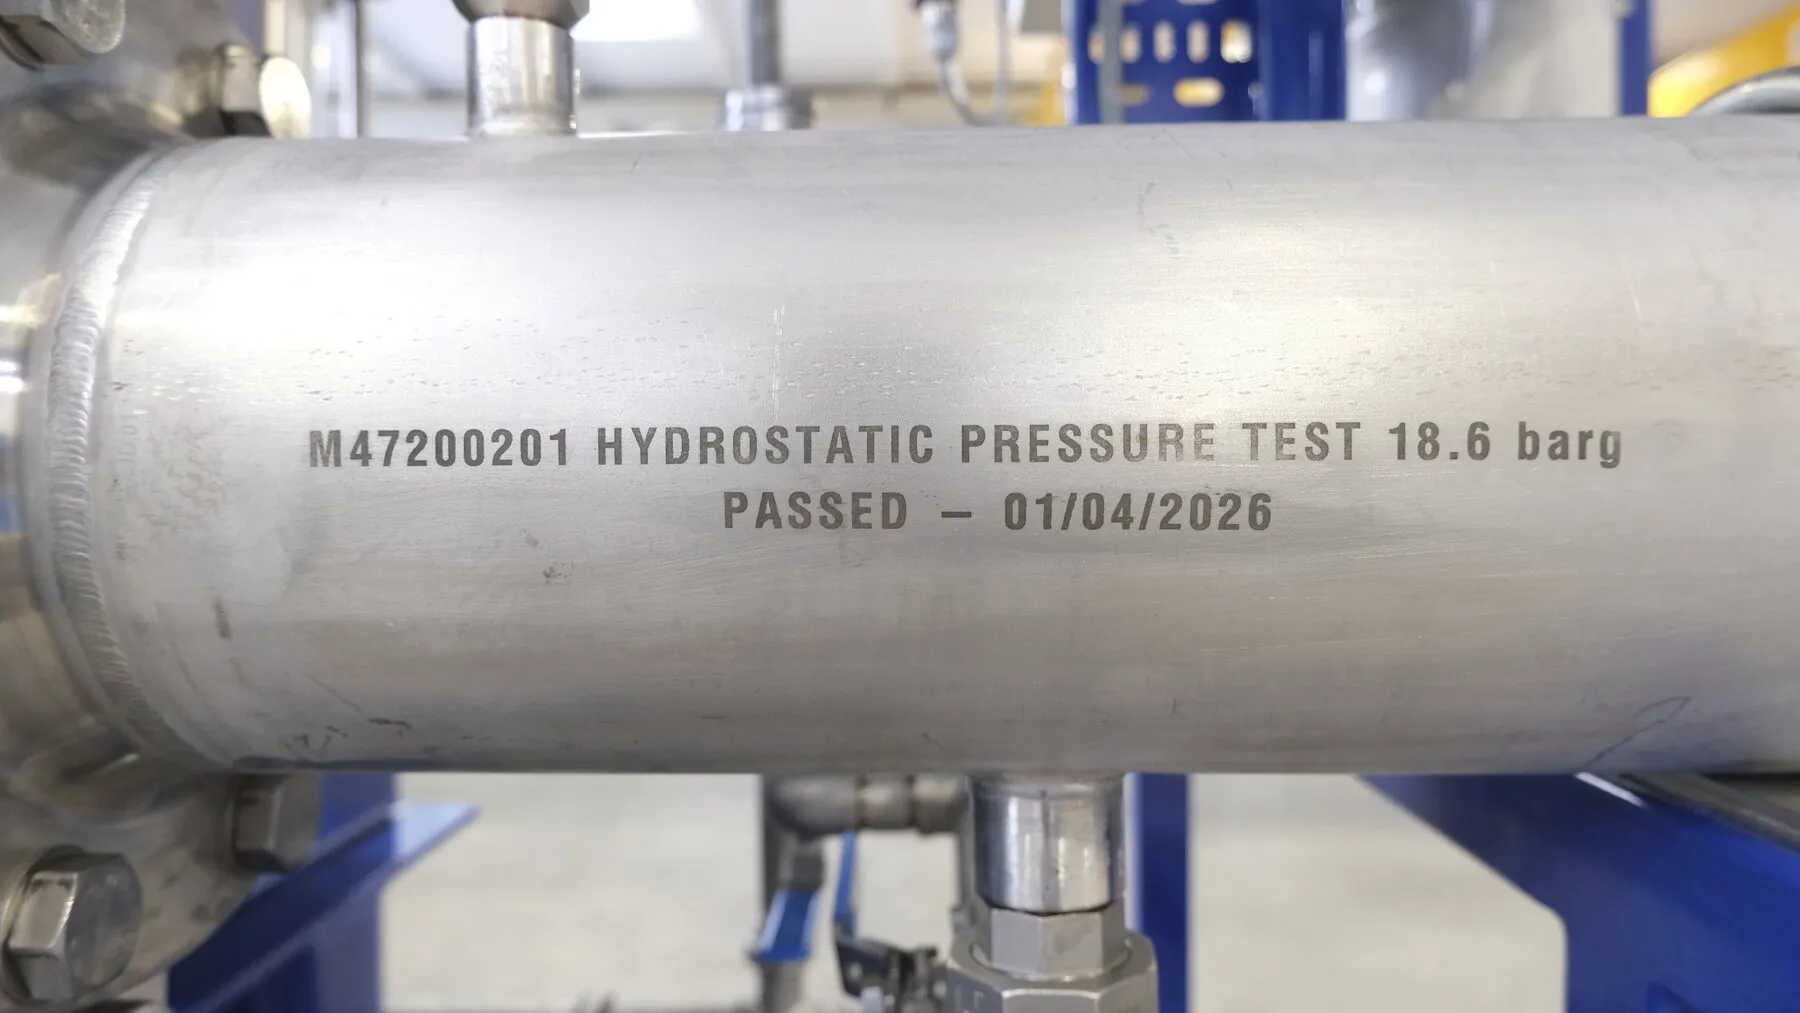
- Hydrostatic tests on the components with a 30-minute hold and no pressure drop
- Service test on the three assembled skids at design pressure
- Dimensional inspection of every component
03
Cleaning and traceability
Spools degreased and flushed internally, welds pickled and passivated, surfaces and flanges protected until delivery. Every component carries a number linking it to the drawing and to the material and test certificates.